 Tiếng
Việt
 Tiếng
Anh
 Tiếng
Nhật


 Tiếng Anh


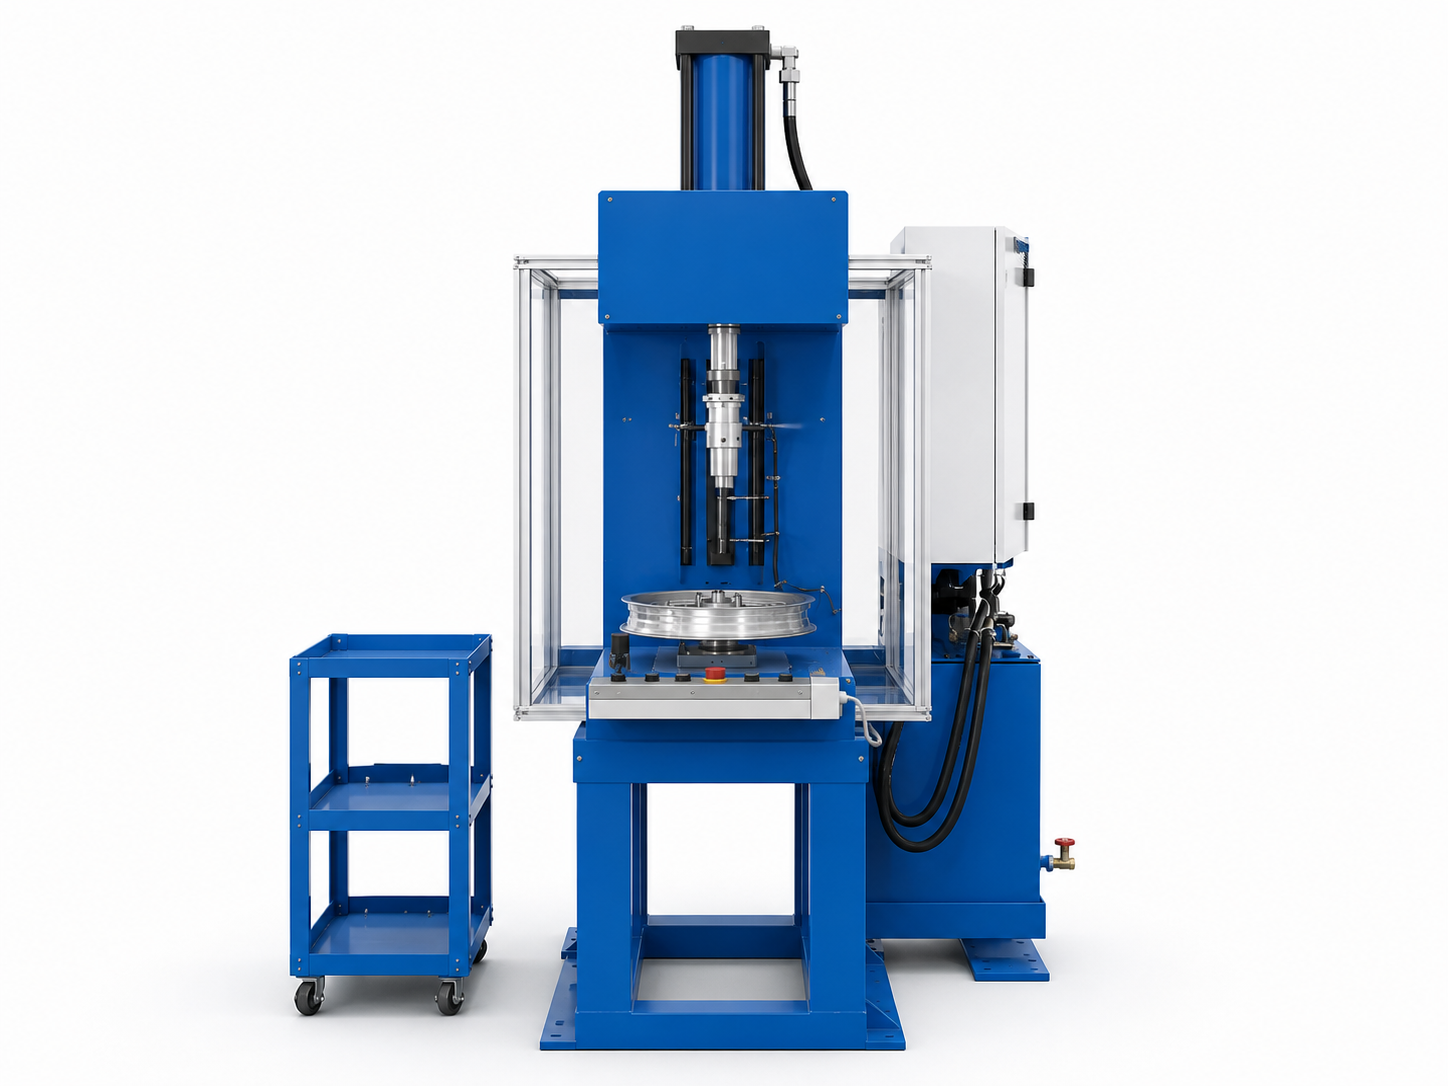
The machine presses the ball into the rim
The machine presses the ball into the rim is a specialized hydraulic press widely used in the automotive and motorcycle manufacturing and assembly industries. The machine is designed to automatically press bearings into motorcycle and automobile wheel rims, as well as perform other press-fit assembly applications in production facilities. It ensures high assembly accuracy while improving production efficiency. The workpieces include bearings and wheel rims for motorcycles and automobiles. With a fully automated and safe operating cycle, the machine helps optimize assembly line productivity while simplifying operation for workers.
VIETNAM CNC & TECHNOLOGY APPLICATION JOINT STOCK COMPANY
Hotline: +84.916 63 9355 / +84.915 74 4664
Email: Sales01@cncvina.com.vn / Sales03@cncvina.com.vn
Product description

The machine presses the ball into the rim is a specialized solution designed to automate the process of pressing bearings into wheel rims, ensuring high precision and consistent performance. The machine uses a hydraulic pressing system combined with fixtures and sensors to control the pressing process. With a cycle time of approximately 5 seconds per assembly, it is well suited for continuous production and high-volume manufacturing. The machine features a robust structure, safe operation, and can be configured for either automatic or manual operation depending on production requirements. Using this machine helps reduce manual operations, minimize assembly errors, and improve product consistency. It is an ideal solution for motorcycle assembly lines and other manufacturing processes requiring precise bearing press-fitting. In the following article, CNC VINA will provide a detailed overview of the machine’s structure, operating principle, and operation process.
Technical specifications of the machine presses the ball into the rim
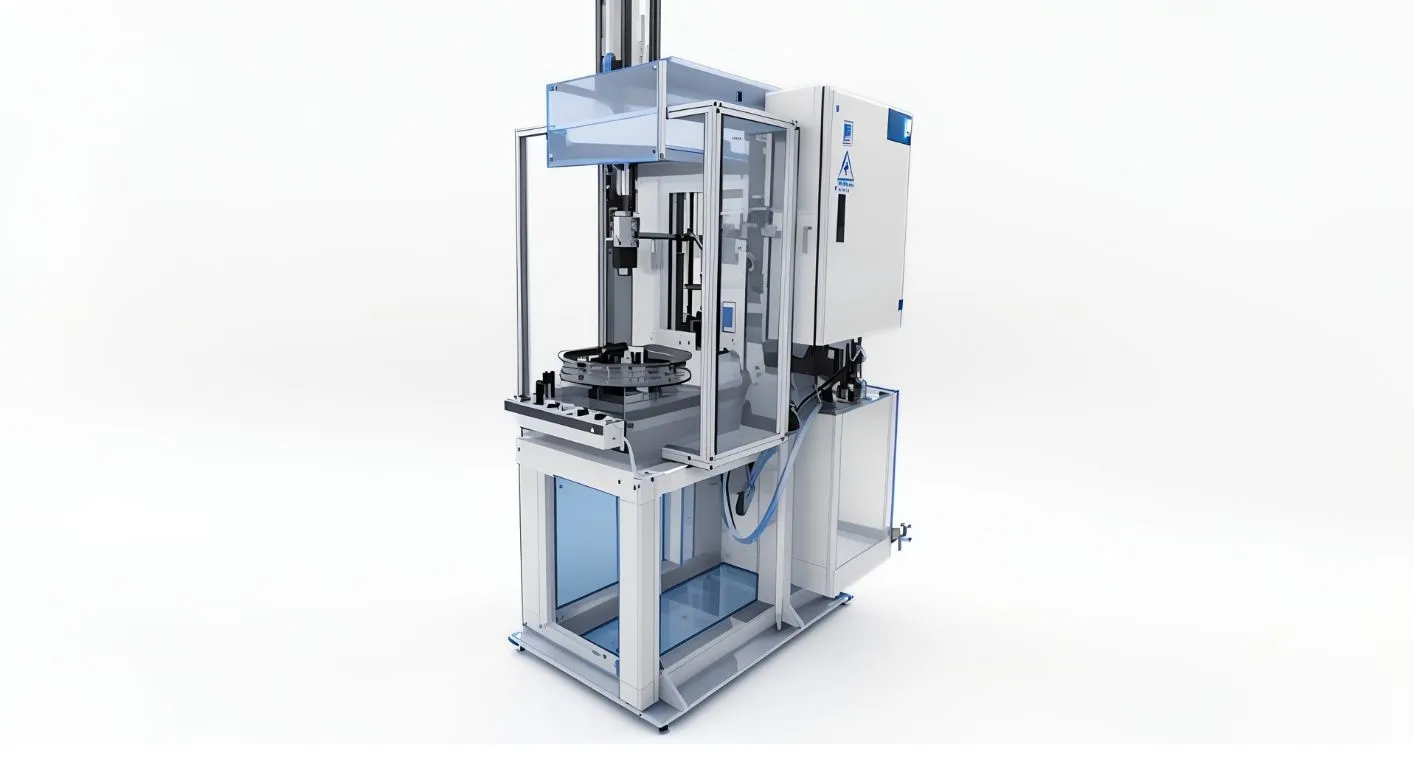
| Machine dimensions | L1200 × W1090 × H1470 mm |
| Power supply | AC 380 V – 50 Hz, 3-phase |
| Control voltage | DC 24 V |
| Power | 5 kW |
| Weight | 520 kg |
| Cycle time | 5 seconds/assembly |
| Control system | Control cabinet + operation buttons |
| Color | Optional |
Structure of a hydraulic press that presses bearings onto the rim
The hydraulic wheel rim bearing press machine is designed with a relatively simple structure, focusing on the main functional units required to accurately position and press bearings into wheel rims. The machine consists of five main units:
- Hydraulic unit: This unit generates and transmits the pressing force, including the hydraulic pump, oil tank, hydraulic piping, control valves, and hydraulic cylinder. During operation, the hydraulic system supplies the appropriate pressure to the cylinder, generating the pressing force required to install the bearing into the wheel rim accurately and stably.
- Machine frame and base: This is the main load-bearing structure of the machine, supporting the hydraulic unit, pressing unit, fixtures, and other components. The machine is built with a rigid structure to minimize vibration and deformation during pressing, thereby maintaining stability and accuracy throughout each operating cycle.
- Fixture unit: The fixture is responsible for positioning and securing the wheel rim and bearing before the pressing operation. It is designed according to the shape of the workpiece to ensure that the wheel rim and bearing are correctly aligned with the pressing head. This helps ensure accurate pressing while minimizing bearing misalignment, incorrect fixturing, or reversed installation.
- Pressing unit: This unit directly performs the operation of pressing the bearing into the wheel rim. Driven by the hydraulic cylinder, the pressing head moves according to the preset stroke and applies force to the bearing. The pressing unit works together with the fixture and sensor system to ensure that the pressing operation is performed at the correct position and according to the required technical specifications.
- Control system: The control system includes the electrical control cabinet, operation buttons, and sensor system. The operator can select automatic or manual operation depending on production requirements. Two-hand operation buttons help keep the operator outside the hazardous area when starting the pressing cycle, while the sensors monitor the machine and workpiece status during operation.
Operating principle and operation guide for the machine presses the ball into the rim
The wheel rim bearing press machine uses a hydraulic system combined with fixtures and sensors to perform the bearing pressing process accurately and consistently. The following section explains the machine’s operating principle and basic operating steps.
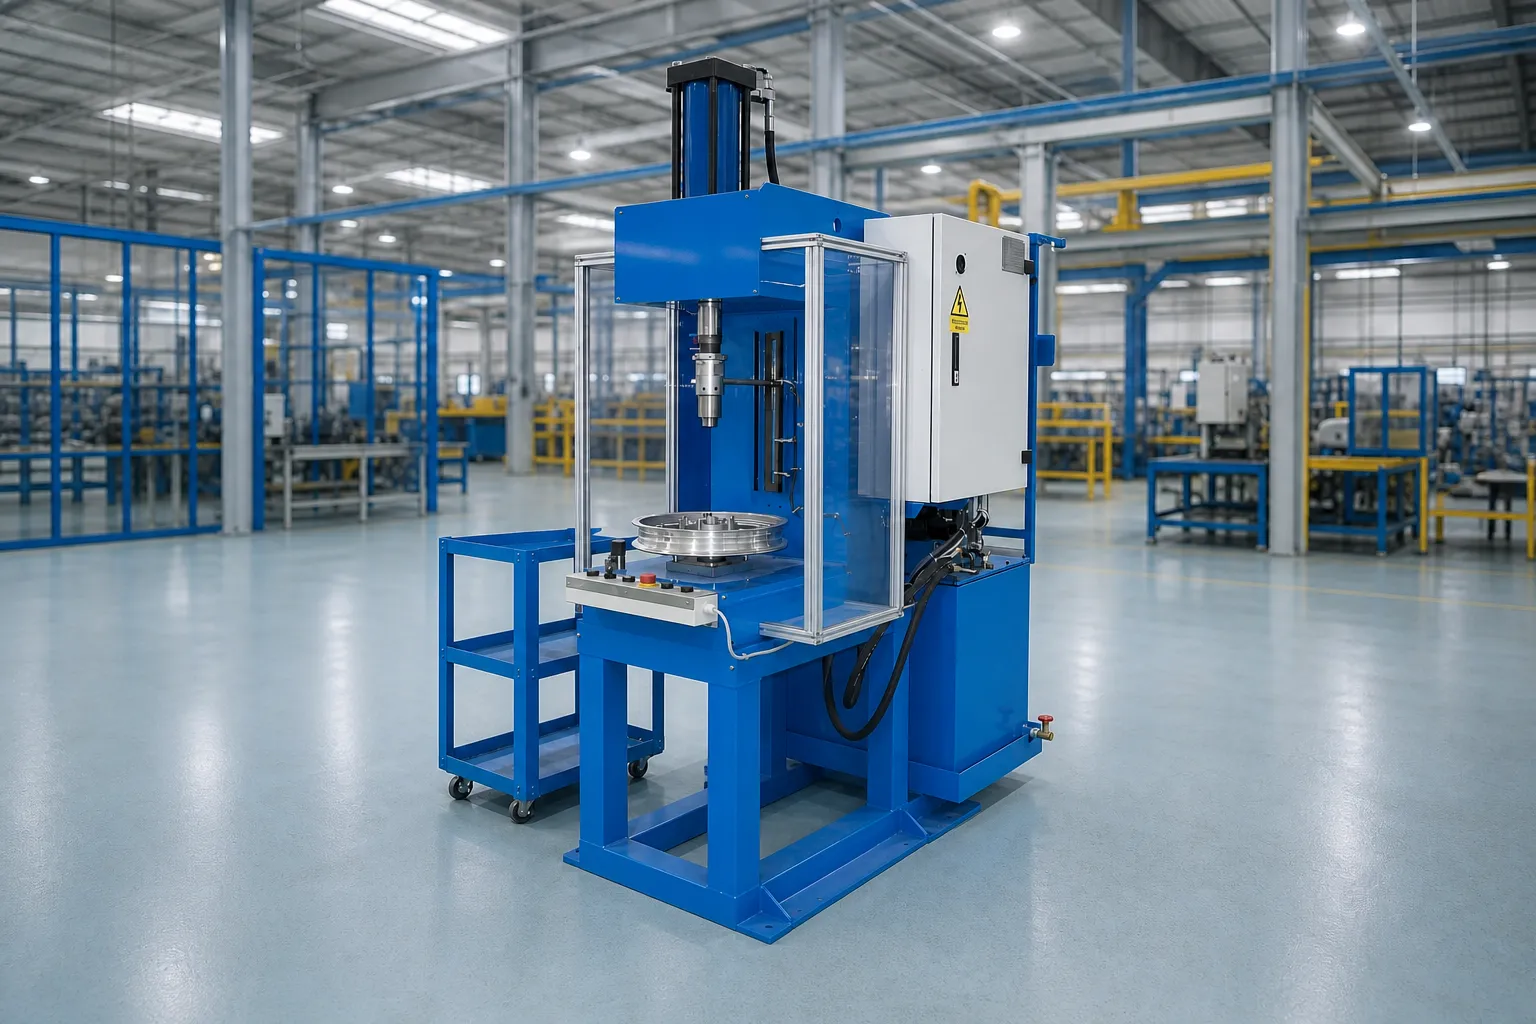
Operating principle of the hydraulic wheel rim bearing press machine
The wheel rim bearing press machine operates based on a hydraulic system that generates the pressing force, combined with positioning fixtures and a sensor system to press the bearing into the correct position on the wheel rim. The entire process is controlled step by step to ensure accuracy and consistency while reducing assembly time.
Step 1: Place the wheel rim into the fixture
Before starting the cycle, the operator places the wheel rim into the dedicated fixture on the machine table. The fixture positions and securely holds the wheel rim, ensuring that the center and bearing installation position are correctly aligned with the pressing head.
Step 2: Place the bearing onto the pressing head
The bearing is placed onto the pressing head of the hydraulic cylinder. A magnetic holder is used to secure the bearing on the pressing head, preventing it from falling or shifting as the machine moves into the pressing position.
Step 3: Confirm the position and pressing conditions
After the wheel rim and bearing are properly positioned, the sensor system checks the status and position of the workpiece. The sensors confirm that the necessary conditions are met before the machine starts the cycle and help detect incorrectly positioned or reversed workpieces. The pressing operation is only enabled when the required safety and positioning conditions have been confirmed. This system helps minimize errors caused by incorrect workpiece positioning.
Step 4: Activate the pressing cycle
The operator presses the two control buttons simultaneously to start the cycle. Once the control signal is received, the hydraulic system supplies oil to the cylinder, causing the pressing head to move according to the preset stroke.
The pressing head applies force to the bearing and presses it into the designated position on the wheel rim. The pressing force is adjusted using a manual adjustment valve according to the requirements of each process, while the pressing stroke is controlled by a proximity sensor system.
Step 5: Control the pressing stroke and time
During the pressing process, the sensor system monitors the position of the pressing mechanism to ensure that the pressing head moves through the correct stroke. When the preset position is reached, the pressing process is completed or proceeds to the next step of the cycle.
In addition, the force-holding time can be set using an external timer. Controlling the pressing force, stroke, and pressing time simultaneously helps ensure stable and consistent bearing installation across products.
Step 6: Return the pressing head to its initial position
After the bearing has been fully pressed into the wheel rim, the hydraulic cylinder retracts, returning the pressing head to its original position. At this point, the pressing cycle is complete and the bearing has been installed.
Step 7: Remove the product and start the next cycle
The operator presses the finish button, removes the completed wheel rim from the fixture, and performs a quick check of the bearing installation position. The next wheel rim is then placed into the fixture and a new bearing is positioned on the pressing head to start the next cycle. According to CNC VINA's published specifications, the machine has a cycle time of approximately 5 seconds per assembly, making it suitable for high-productivity production lines.
Operation guide for the wheel rim bearing press machine
Before operating the hydraulic wheel rim bearing press machine, the operator should pay attention to the following points:
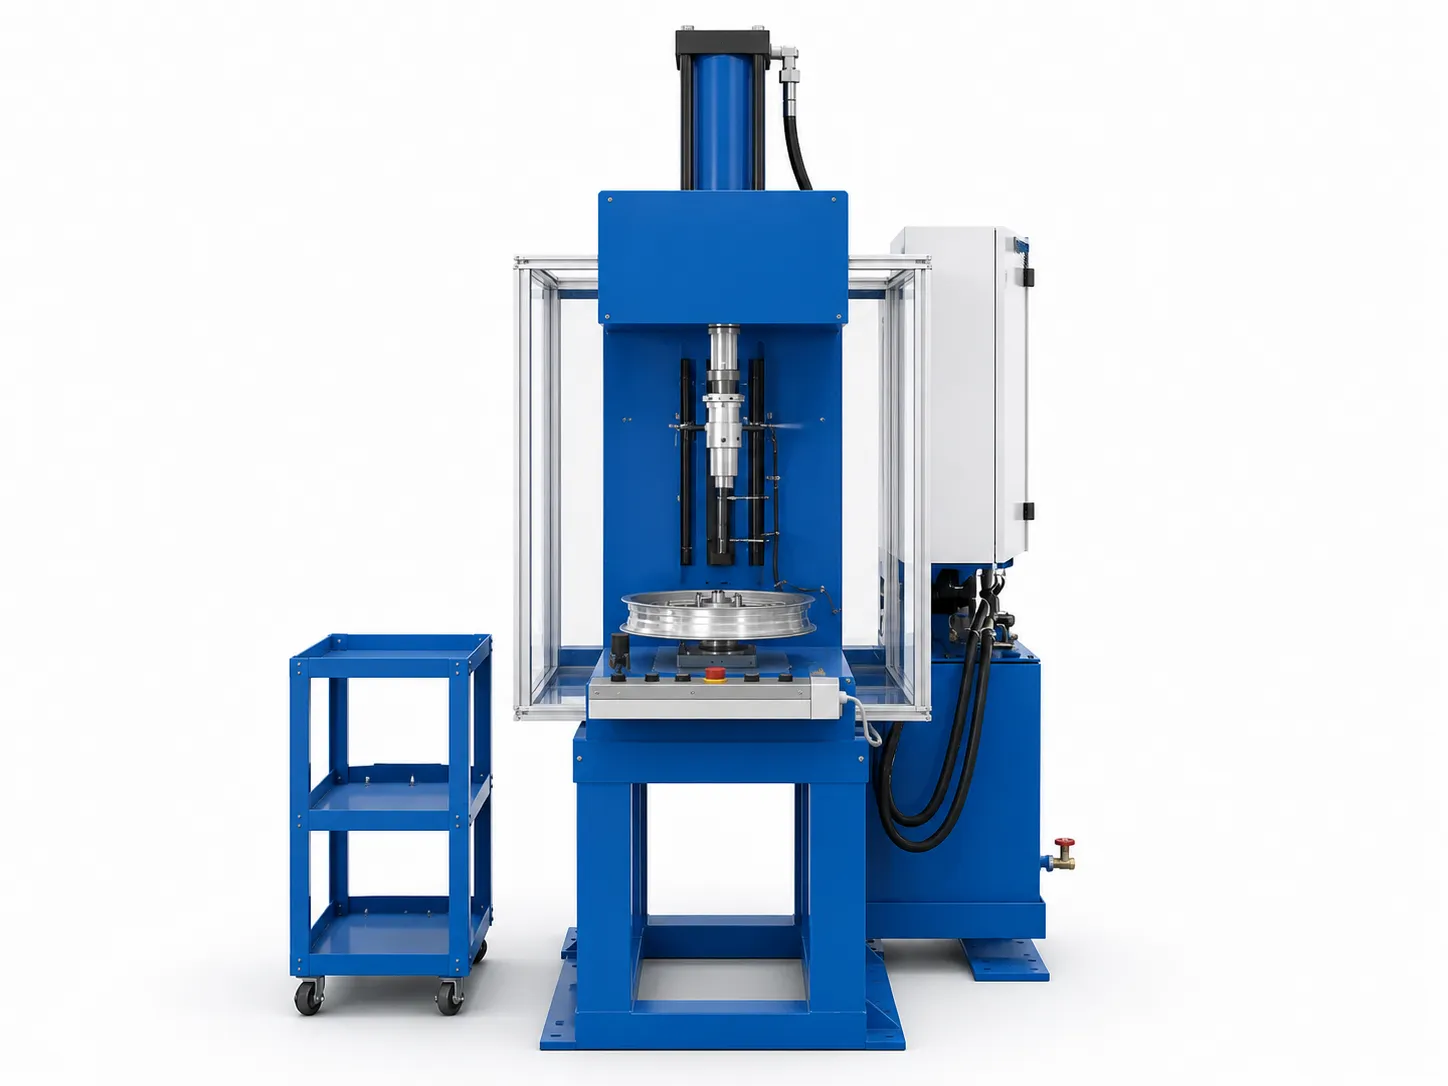
- Check the machine before operation: Before starting, check the power supply, hydraulic system, operating pressure, condition of the hydraulic cylinder, pressing head, fixture, and sensor system. Make sure the working area is free of obstructions and that all safety devices are functioning properly.
- Set the pressing parameters: Set the required parameters, including pressing force, pressing stroke, and force-holding time, according to the product requirements. The parameters should be adjusted to suit the size and characteristics of the bearing and wheel rim.
- Place the wheel rim into the fixture: Position the wheel rim correctly in the fixture and check that it is securely held. Ensure that the wheel rim is accurately positioned before starting the pressing cycle.
- Place the bearing onto the pressing head: Position the bearing on the pressing head or bearing-holding mechanism according to the machine design. Check that the bearing is properly aligned before starting the pressing operation.
- Activate the pressing cycle: After checking the workpiece and confirming the safety conditions, the operator presses the two control buttons simultaneously to activate the cycle. The machine then performs the pressing operation according to the preset parameters.
- Inspect the product after pressing: After the pressing head returns to its initial position, remove the product from the fixture and check the bearing installation position. If the product meets the requirements, proceed with the next product. If the bearing is misaligned or not pr
Key fatures of the hydraulic wheel rim bearing press machine
The machine presses the ball into the rim is a specialized solution designed to press bearings into wheel rims quickly, accurately, and consistently. The machine uses a hydraulic pressing mechanism combined with fixtures and sensors, making it suitable for assembly processes in industrial manufacturing.
- Robust machine structure: The machine features a rigid structure designed to withstand hydraulic pressing forces. Its high structural rigidity helps minimize vibration and maintain stability throughout the pressing process.
- Safe operation: The machine is equipped with a safety sensor system to monitor the status of the pressing head and hydraulic cylinder. Two-hand operation buttons allow the operator to start the cycle from a safe position, helping reduce the risk of contact with the pressing area during operation.
- Flexible automatic and manual operation: The wheel rim bearing press machine can be configured for either automatic or manual operation depending on the requirements of each production line.
- Suitable for continuous production: Automatic operation is suitable for continuous production processes, reducing operator intervention and maintaining a stable working cycle. Manual operation is convenient for machine inspection, parameter setup, mechanism adjustment, and maintenance.
- Sensor system for detecting incorrect positioning: The integrated sensor system checks the condition and position of the workpiece before the pressing cycle begins. If the wheel rim is incorrectly positioned or installed in reverse, the system can detect the abnormal condition and prevent the pressing operation. This feature helps minimize errors caused by incorrect workpiece positioning while protecting the product, fixture, and pressing mechanism.
- High productivity and short cycle time: The machine has a cycle time of approximately 5 seconds per assembly, making it suitable for high-volume and continuous production. Automating the positioning and bearing pressing process helps reduce manual operations, shorten production cycles, and maintain consistent product quality. Depending on production requirements and output targets, CNC VINA can customize and adjust the machine to suit each production line.

Piaggio motorcycle rims are pressed with ball bearings on CNC VINA hydraulic presses
Operation and maintenance of the motorcycle wheel rim bearing press machine
To ensure stable and safe operation and maintain long-term performance, the motorcycle wheel rim bearing press machine must be operated correctly and maintained regularly. Operators should follow the technical instructions provided with the machine and regularly inspect the hydraulic, electrical, and mechanical systems during operation.
- The operator places the wheel rim into the dedicated fixture on the machine table and positions the bearing for pressing.
- The bearing is placed onto the pressing head of the hydraulic cylinder and securely held by a magnetic holder to prevent movement during the pressing process.
- After the wheel rim and bearing are correctly positioned, the sensor system checks the required conditions before the cycle begins.
- The operator presses the two control buttons simultaneously to activate the machine. The hydraulic cylinder moves the pressing head and presses the bearing into the wheel rim.
- Once the pressing stroke is completed, the pressing head and hydraulic cylinder return to their initial positions. The operator presses the finish button, removes the completed product from the fixture, and loads a new product for the next cycle.
CNC VINA develops specific operating procedures and safety guidelines for each specialized machine according to the requirements of each customer and production process. Operators should follow the parameters specified in the technical documentation provided with the machine, including:
- Pressing force: Adjusted using a manual adjustment valve according to the technical requirements of each process.
- Pressing stroke: Controlled by the proximity sensor system to determine the end position of the pressing mechanism.
- Pressing time: Set using an external timer to ensure an appropriate force-holding time for each product.
In addition, to maintain stable operation and minimize production interruptions, operators should regularly inspect the machine's functional units, particularly the hydraulic system, power supply, hydraulic cylinder, sensors, and pressing mechanism.
- After each shift, the machine should be cleaned to remove dust, dirt, and oil or grease buildup from the necessary areas. Mechanical assemblies should also be inspected and lubricated periodically according to technical requirements to reduce friction, minimize wear, and maintain stable machine operation.
- Proper operation, inspection, and regular maintenance not only help ensure operator safety but also extend equipment service life, maintain pressing accuracy, and reduce machine downtime caused by unexpected issues.
The machine presses the ball into the rim is an effective solution for businesses looking to improve efficiency and stability in their assembly processes. Integrating the machine into the production line reduces dependence on manual operations and helps maintain consistent productivity. The machine can be designed and customized according to product characteristics and the specific requirements of each production line. In addition to improving productivity, it also helps control product quality and minimize errors during bearing installation. This makes it a suitable automation solution for motorcycle manufacturing and assembly plants as well as mechanical component production. CNC VINA provides customized machine design and manufacturing solutions to meet the specific requirements of each production process.
VIETNAM CNC & TECHNOLOGY APPLICATION JOINT STOCK COMPANY
Factory: Song Cung Industrial Site, Dong Thap Commune, Dan Phuong District, City. Hanoi Vietnam
Phone: +84.916 63 9355 / +84.915 74 4664
Website: https://cncvina.com.vn; https://cncvina.net; https://cncviname.com.vn
Email: Sales01@cncvina.com.vn | Sales03@cncvina.com.vn


